
Ceramic Slurry
TEL:18925129293


Ceramic Slurry, Bubbles Eliminated Completely! Measured Density Test
date:2026-09-14author:小施Ceramic Slurry, Bubbles Eliminated Completely! Measured Density Test
From tape casting, slip casting to spraying, defoaming solutions for full-range slurries of electronic ceramics, structural ceramics and functional ceramics
Ceramic Slurry is a high solid-loading suspension system composed of ceramic powder (alumina, zirconia, silicon carbide, barium titanate, PZT, etc.) and organic carriers (binder, dispersant, plasticizer, solvent) via ball milling or stirring mixing. It is widely applied in tape casting (MLCC/substrates), slip casting (structural parts), hot die casting (precision components), ceramic spraying, gel-casting and other processes. Entrapped bubbles inside ceramic slurry will directly induce defects such as pores, uneven density, dielectric layer fracture and bending deformation after sintering, which greatly impair the dielectric properties and breakdown voltage of electronic ceramics as well as mechanical strength of structural ceramics. SIENOX provides complete solutions from powder dispersion to vacuum defoaming for various ceramic slurries through self-developed planetary stirring defoaming technology.
◆ Material Properties
Common Ceramic Powders Al₂O₃, ZrO₂, SiC, BaTiO₃, PZT, AlN, Si₃N₄ | Organic Carrier Systems PVB/Methyl Ethyl Ketone tape casting system, PEG/Glycerol slip casting system, paraffin hot die casting system, acrylic dispersion system | Solid Content Range 40~65vol% (tape casting slurry:45~55vol%, slip casting slurry:35~50vol%, hot die casting:55~65vol%) |
Slurry Viscosity Range 50~150,000 cps (tape casting slurry:50~500cps, slip casting:1,000~20,000cps, hot die casting:50,000~150,000cps) | Powder Particle Size D50=0.2~5μm (submicron for electronic ceramics) to D50=5~50μm (structural ceramics) | Typical Application Scenarios Tape Casting, Slip Casting, Hot Die Casting, Gel-Casting, Ceramic Spraying |
◆ Mature Application Fields
📱 MLCC Multilayer Ceramic Capacitor BaTiO₃ barium titanate tape casting slurry, dielectric layer thickness 1~10μm, slurry viscosity 50~300cps. Bubbles directly affect dielectric layer integrity and breakdown voltage. | 🔌 Ceramic Substrate & Packaging Al₂O₃/AlN alumina or aluminum nitride tape casting slurry for IGBT substrates and LED heat dissipation substrates. Slurry viscosity 200~800cps, high thermal conductivity and insulation required. | 🦷 Zirconia Dental & Medical Ceramics 3Y-TZP zirconia slip casting or gel-casting slurry for dental crowns, implants and artificial joints. Slurry viscosity 5,000~30,000cps, high density and biocompatibility required. |
📡 Piezoelectric Ceramic Components PZT lead zirconate titanate tape casting or slip casting slurry for ultrasonic transducers, filters and actuators. Slurry viscosity 1,000~10,000cps, bubbles affect polarization uniformity. | 🔧 Structural Wear-resistant Ceramic Parts Al₂O₃/SiC alumina or silicon carbide slip casting slurry for sealing rings, bearings, liners and nozzles. Slurry viscosity 3,000~20,000cps. | 🔋 Solid-State Battery Ceramic Electrolyte LLZO/LLZTO solid electrolyte ceramic slurry, tape-cast for thin electrolyte films. Slurry viscosity 100~2,000cps, bubbles cause ionic conduction interruption. |
🏭 Industrial Ceramic Coatings Al₂O₃/ZrO₂ ceramic spraying suspension for thermal barrier coatings and wear-resistant coatings on aero-engine blades. Slurry viscosity 500~5,000cps. | 🔥 High-Temperature Kiln Furniture & Refractories Mullite/corundum slip casting slurry for shelves, saggers and crucibles. Slurry viscosity 5,000~15,000cps, good thermal shock resistance and long service life required. | 🎓 Scientific Research & New Material Development New ceramic formula development and process parameter verification for universities and research institutes. Small-batch slurry preparation and defoaming test, unlimited viscosity range, free sample testing available. |
◆ Core Problems Caused by Bubbles
⚠️ Porosity & Insufficient Density After Sintering Bubbles in the slurry leave voids during drying and sintering, reducing sintered body density. Electronic ceramics require relative density ≥97% (MLCC ≥99%). Residual bubbles directly lead to deviation of dielectric constant and decreased breakdown voltage. | ⚠️ Dielectric Layer Fracture & Electrical Failure For thin-layer devices such as MLCC, a single bubble can cause penetrating defects in micron-scale dielectric layers, resulting in short circuit or insulation failure. Every 0.1% increase of gas content in tape casting slurry may multiply the defect rate. |
⚠️ Uneven Shrinkage, Warpage & Cracking Uneven bubble distribution leads to inconsistent shrinkage in each area of the green body. Internal stress concentration occurs during drying and sintering, triggering warping deformation or even penetrating cracks, making dimensional accuracy uncontrollable. | ⚠️ Surface Pinholes & Deteriorated Surface Finish Bursting bubbles on the slurry surface form pinholes and pits, raising surface roughness of cast films and cast parts. Subsequent grinding & polishing costs rise, and severe cases lead to direct scrapping. |
◆ Recommended Process — Planetary Stirring Defoaming
Step 1 Pre-Dispersion of Powder Add ceramic powder into organic carriers (binder + solvent + dispersant) in batches. Carry out low-speed pre-stirring to preliminarily wet powder and avoid dry powder agglomerates trapping air. | Step 2 Ball Milling / High Speed Dispersion Ball milling or high-speed dispersion brings powder particle size to target D50, meanwhile powder fully mixes with carriers. A large amount of air will be entrapped in this stage and slurry gas content rises significantly. |
Step 3 Vacuum Stirring Defoaming Start planetary stirring under -95KPa vacuum. Revolution plus rotation continuously flips slurry. Bubbles expand, float up and rupture, removing most entrapped gas within 3~8 minutes. | Step 4 Direct Tape Casting / Slip Casting After Defoaming Break vacuum and discharge directly into tape caster or slip casting process. No container transfer required to prevent secondary air entrapment. Fully closed operation keeps slurry gas content stable and controllable. |
◆ Recommended Equipment
MIX60 — Laboratory-grade planetary stirring defoaming machine, single batch capacity 5~60g. Suitable for electronic ceramic slurry formula development and tape casting parameter verification, supports -95KPa vacuum defoaming.
MIX90 — Pilot-scale stirring defoaming machine, single batch capacity 200~900g. Suitable for medium-viscosity ceramic slurries (≤80,000cps) batch preparation, universal model for structural & piezoelectric ceramics.
MIX1000PLUS — Large-capacity flagship model, max single batch capacity 2000g. Specialized for high solid loading & high viscosity ceramic slurries (≤200,000cps), suitable for mass production of MLCC/substrate slurries.
MIX2000 — Industrial mass production model, single batch capacity over 2000g. Matched with automatic loading & unloading system to meet mass production cycle requirements of ceramics.
◆ Test Cases
▶ Case 1: BaTiO₃ Barium Titanate MLCC Tape Casting Slurry
Test Material | BaTiO₃ barium titanate powder (D50=0.3μm) + PVB/Methyl Ethyl Ketone tape casting system, solid content 50vol% |
Slurry Viscosity | Approx. 150 cps |
Test Model | MIX60 |
Vacuum Degree | -95KPa |
Rotation Speed | Revolution 1500rpm / Rotation 1000rpm |
Treatment Time | 3 minutes |
Treatment Temperature | Room temperature (25℃), sealed & protected from light |
✅ Defoaming Result: Cross-section porosity of tape casting slurry <0.3%, thickness uniformity of cast film ±1.5%, relative density after sintering ≥99.2%, breakdown voltage >15KV/mm, dielectric loss tanδ<0.02. It meets the integrity requirements of dielectric layers for high-capacity MLCC.
▶ Case 2: Al₂O₃ Alumina Structural Ceramic Slip Casting Slurry
Test Material | Al₂O₃ alumina powder (D50=8μm) + PEG/Glycerol water-based slip casting system, solid content 55vol% |
Slurry Viscosity | Approx. 5,000 cps |
Test Model | MIX90 |
Vacuum Degree | -95KPa |
Rotation Speed | Revolution 1800rpm / Rotation 1200rpm |
Treatment Time | 5 minutes |
Treatment Temperature | Room temperature (25℃) |
✅ Defoaming Result: Cross-section porosity of slip cast green body <0.5%, no cracking after drying, relative density after sintering ≥98.5%, bending strength ≥380MPa, Vickers hardness HV12.5, no surface pinhole defects. Meets requirements of structural parts such as sealing rings and bearings.
▶ Case 3: ZrO₂ Zirconia Dental Ceramic Gel-Casting Slurry
Test Material | 3Y-TZP zirconia powder (D50=0.5μm) + acrylamide monomer gel-casting system, solid content 58vol% |
Slurry Viscosity | Approx. 2,000 cps |
Test Model | MIX90 |
Vacuum Degree | -95KPa |
Rotation Speed | Revolution 2000rpm / Rotation 1500rpm |
Treatment Time | 5 minutes |
Treatment Temperature | Room temperature (25℃), operation away from light |
✅ Defoaming Result: Cross-section porosity of gel-cast green body <0.3%, relative density after sintering ≥99.5%, bending strength >1000MPa, fracture toughness KIC>8MPa·m^1/2, good light transmittance. Satisfies mechanical and aesthetic requirements of dental all-ceramic crowns and bridges.
◆ Comparison Before & After Improvement
Comparison Item | Hand Mixing / Atmospheric Mixing | Static Vacuum Defoaming Tank | SIENOX Planetary Stirring Defoaming |
Slurry Porosity | 3~10% | 1~3% | <0.3% |
Relative Density After Sintering | 90~95% | 95~98% | ≥99% |
Powder Dispersion Uniformity | Severe agglomeration, uneven distribution | No improvement for dispersion, only gas removal | Uniform dispersion without agglomeration |
Tape Cast Film Thickness Uniformity | Deviation ±5~10% | Deviation ±3~5% | Deviation ±1.5% |
Yield Rate | 55~70% | 80~90% | >98% |
Processing Time | 30~60 minutes (poor effect) | 20~40 minutes (defoaming only) | 3~8 minutes (mixing + defoaming) |
🎯 Free Sample Test
Send us your ceramic slurry samples, we will test defoaming parameters and issue test reports.
Related recommendations
Ceramic Slurry, Bubbles Eliminated Completely! Measured Density Test
Perhaps you still need....
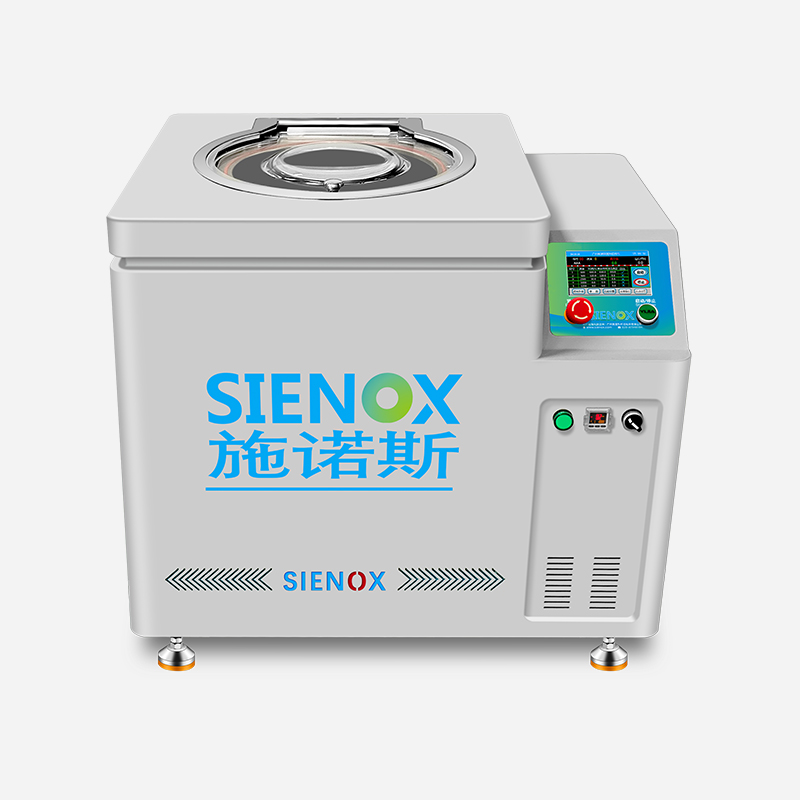
行星式真空脱泡搅拌机 SIE-MIX1000plus
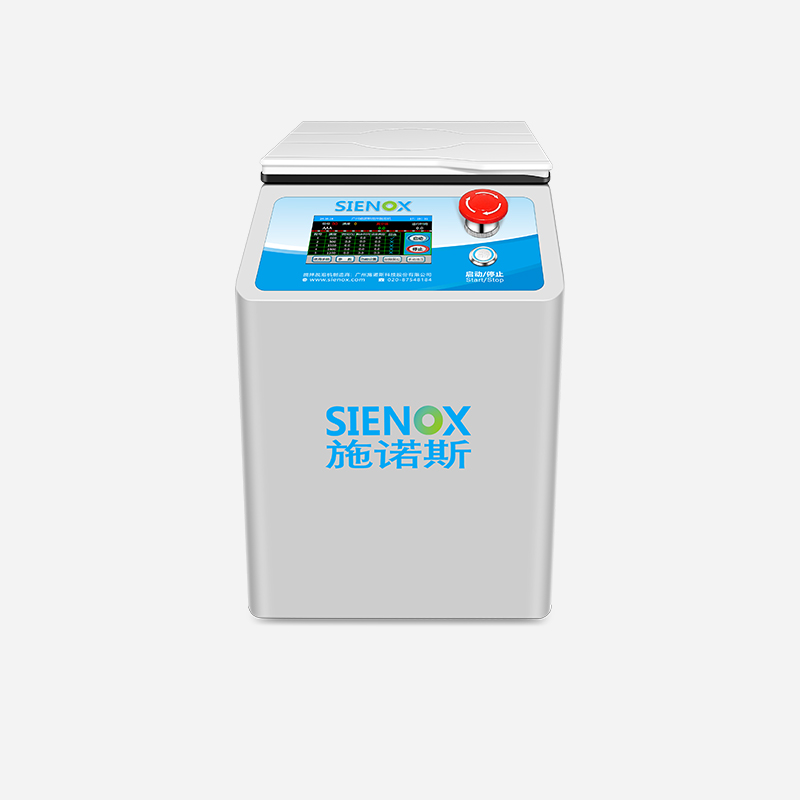
实验室行星式搅拌脱泡机 SIE-CV200
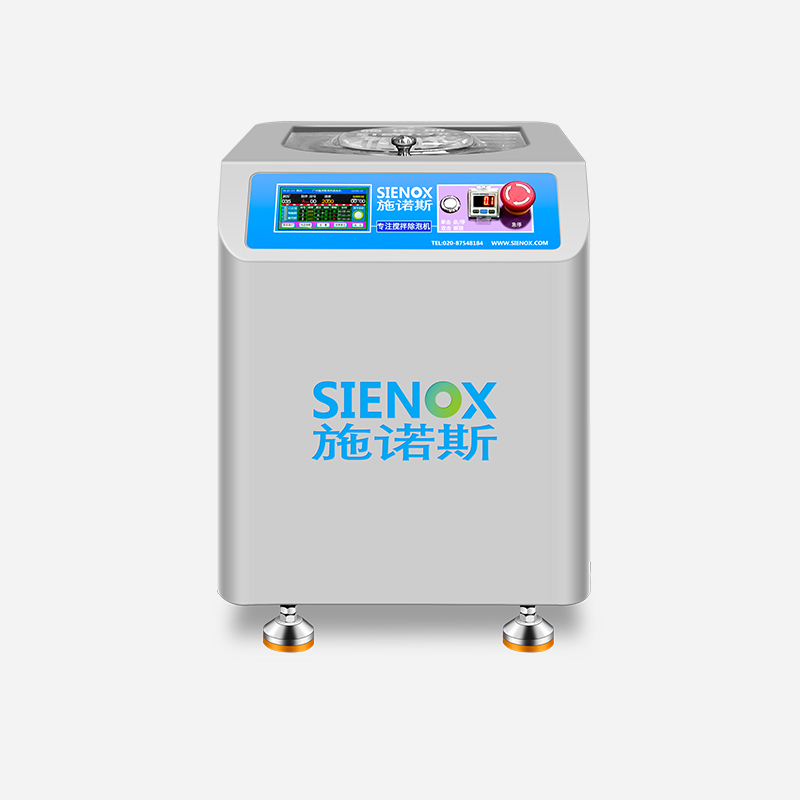
SIENOX行星式脱泡搅拌机 SIE-CV300
离心脱泡机 SIE-C006
About SIENOX
广州施诺斯(SIENOX),20年脱泡机设备研发与生产的源头厂家
超过1800种材料脱泡案例
纳米级脱泡,满足不同材料多段搅拌除泡需要,支持定制
资质齐全,荣获多项国家专利,联系我们可免费试样